

Manual rigging in a steel handling facility wastes time on every single lift. A rigger on the ground, a chain or sling, a hook attachment — then reverse the process at the other end. In a facility completing hundreds of lifts per shift, this labor overhead compounds into a significant operating cost. More critically, every manual rigging cycle puts a person directly beneath a suspended load.
A magnetic overhead crane eliminates both problems. The electromagnet is built into the crane. The operator energizes the magnet from the cabin, picks up the steel load, travels to the deposit point, and releases. No ground crew. No slings. No manual contact with the load. The full cycle is completed by one person from a safe elevated position.
This page covers all three areas you need to make a purchase decision: product design and features, technical parameters, and application scenarios across the industries where magnetic overhead cranes are most commonly used.
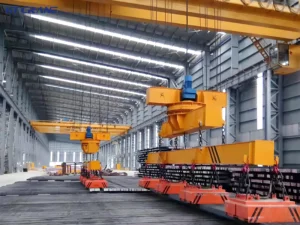
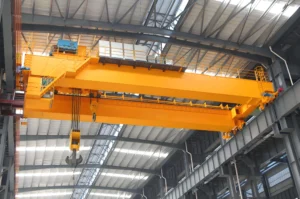
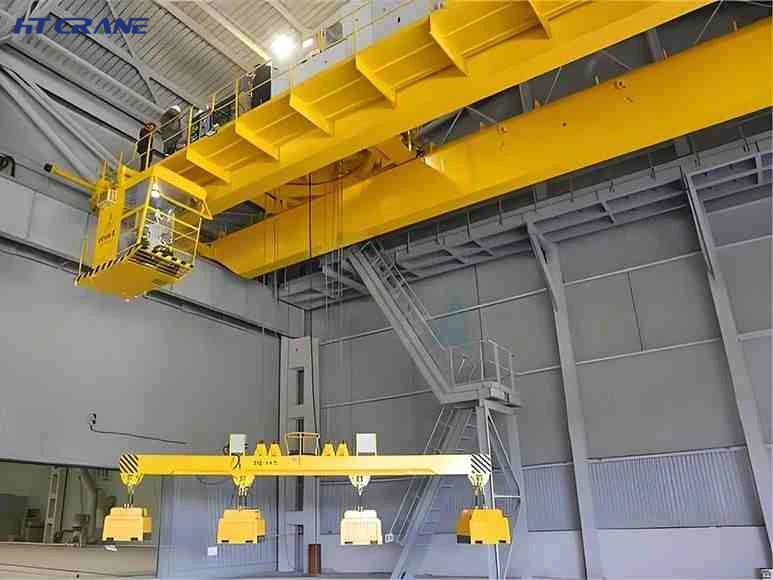
A magnetic overhead crane — classified as QC type under Chinese national standard GB/T 14406 — is a double girder overhead travelling crane with one or more DC electromagnets integrated into the crane trolley as a permanent lifting system. The electromagnet replaces the standard hook and spreader. It is powered by an onboard DC rectifier and controlled directly from the operator’s cabin.
Unlike a standard hook crane fitted with a portable lifting magnet as an add-on, the magnetic overhead crane is designed from the ground up for continuous electromagnetic operation. The rectifier, cabling, magnet suspension, trolley structure, and control system are co-engineered as one integrated machine.
The crane operates as follows: the operator energizes the magnet from the cabin control panel; the magnet generates a DC magnetic field that grips the ferromagnetic load; the crane lifts, travels, and positions the load; the operator de-energizes the magnet to release. The entire cycle requires no ground crew and no manual load attachment.
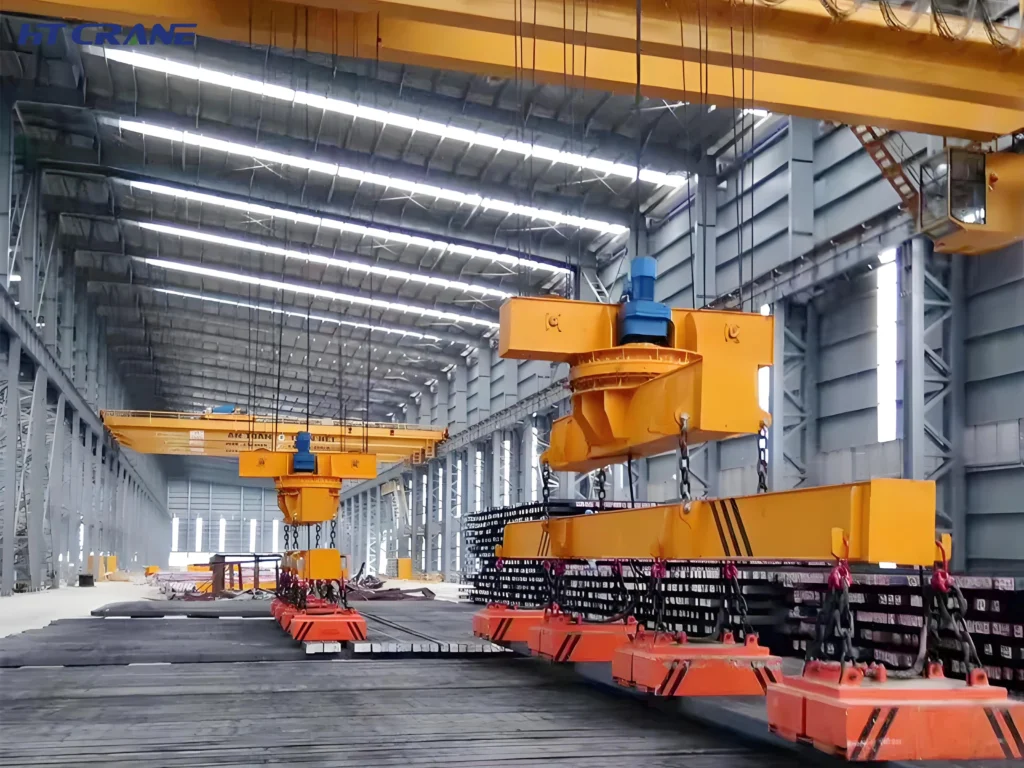
The magnet suspension configuration determines how magnetic force is distributed across the load. Three arrangements are available, each suited to different material handling requirements:
Single magnet on swivel suspension — one large-diameter electromagnet hangs from a swivel hook on the trolley. The swivel allows the operator to rotate the suspended load to the required orientation. Best suited for flat plate, slab, and billet handling where load geometry is consistent and a single pickup point provides adequate grip.
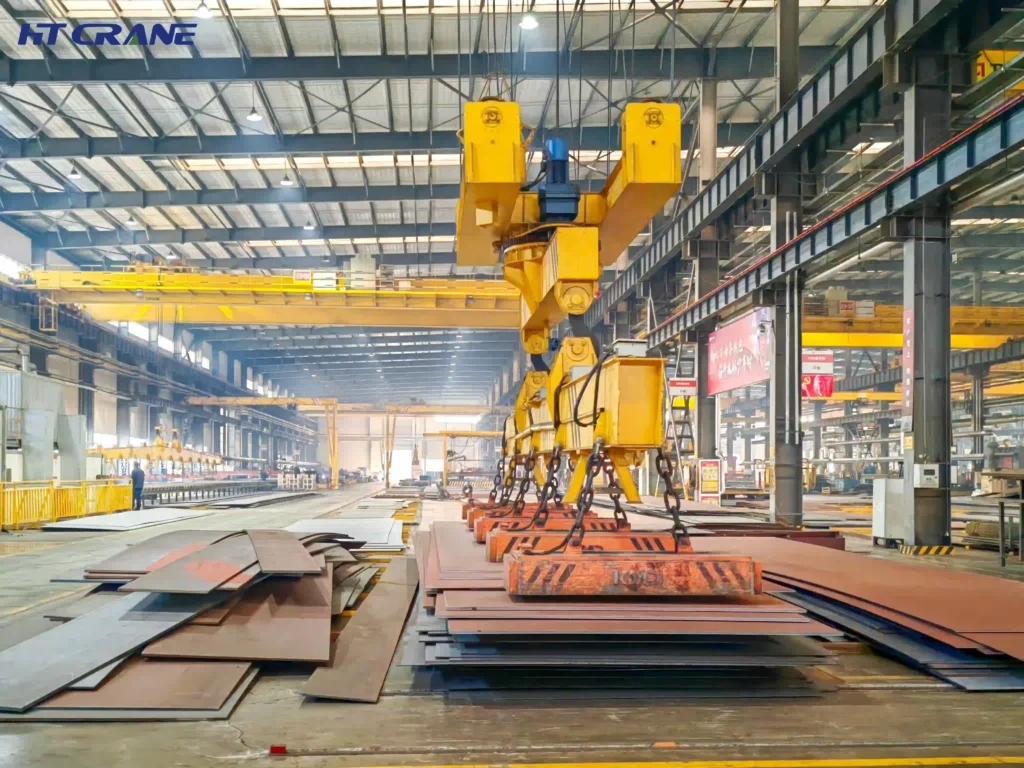
Fixed multi-magnet lifting beam — two or three electromagnets mounted at fixed centres on a rigid beam suspended from the trolley. The beam distributes magnetic force along the length of the load. Used for handling long structural sections — H-beams, channels, rails, and pipe — where a single central magnet would provide inadequate grip across the full load length.
Motorized rotating multi-magnet beam — a powered beam with two or more magnets, with cabin-controlled rotation. The operator rotates the suspended load to the required orientation without repositioning the crane or touching the material. Standard in busy steel service centers where incoming plate orientation must be changed before feeding a processing line.
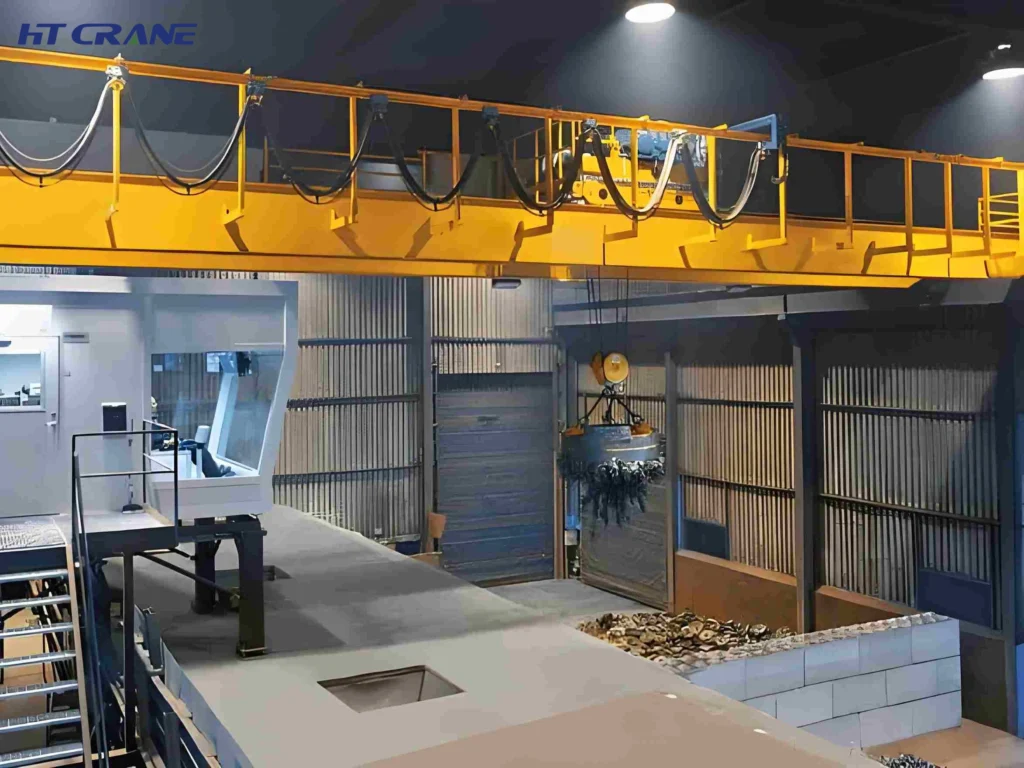
The DC power supply for the electromagnet is a thyristor-type rectifier unit mounted on the crane trolley. It converts the crane’s three-phase AC supply to the DC voltage required by the magnet coil — typically 110V DC or 220V DC depending on magnet size and specification.
The rectifier includes closed-loop current control that maintains consistent magnetic force regardless of supply voltage fluctuation or coil resistance changes with temperature. This is important in high-cycle operations where coil temperature rises during a shift — consistent current means consistent holding force rather than a grip that weakens as the magnet warms up.
If facility mains power fails while the magnet is holding a load, an unprotected electromagnet drops its load instantly. A steel plate falling from height is a serious safety incident — and a crane without battery backup cannot comply with responsible safety standards.
HTcrane magnetic overhead cranes include a battery backup system as standard specification. The battery maintains full magnet energization for a minimum of 30 minutes after mains power failure. This provides the operator with adequate time to lower the load safely to the ground and de-energize the magnet under controlled conditions before backup power is exhausted.
| Parameter | Standard Range |
|---|---|
| Lifting Capacity | 5T – 100T |
| Span | 10.5m – 35.5m |
| Lifting Height | 6m – 20m |
| Work Duty Class | A5 – A7 (GB/T 3811 / ISO 4301) |
| Girder Type | Double girder box section |
| Trolley Type | Metallurgical-grade crab trolley |
| Hoisting Speed | 5 – 20 m/min (full load) |
| Trolley Speed | 20 – 60 m/min |
| Gantry Travel Speed | 40 – 120 m/min |
| Drive System | AC VFD — all motions |
| Control System | PLC with cabin control panel |
| Power Supply | Three-phase AC, conductor rail or festoon |
| Design Standard | GB/T 14406, EN 13001, FEM 1.001 |
| Certification | CE (EU Machinery Directive 2006/42/EC), ISO 9001 |
| Parameter | Specification Range |
|---|---|
| Magnet Diameter | 500mm – 2,000mm |
| DC Supply Voltage | 110V DC / 220V DC |
| Rectifier Type | Thyristor with closed-loop current control |
| Coil Insulation — Standard | Class F (rated to 155°C coil temperature) |
| Coil Insulation — Hot Material | Class H (rated to 180°C coil temperature) |
| Duty Rating — Standard | ED 40% – ED 60% |
| Duty Rating — High Cycle | ED 75% (scrap yard and intensive use) |
| Material Surface Temp — Standard | Up to 100°C |
| Material Surface Temp — Hot Spec | Up to 700°C (metallurgical configuration) |
| Protection Rating | IP54 standard; IP65 for dusty or wet environments |
| Magnet Face Type | Flat (plate and billet); curved (pipe and round bar) |
| Battery Backup | 30 minutes minimum at full load (standard) |
| Battery Monitoring | Real-time cabin display with low-charge alarm |
The magnet’s rated lifting force is always measured on clean, flat, solid steel plate. Real lifting force varies significantly depending on material geometry and surface condition. The table below shows typical achievable force relative to the flat-plate rating:
| Material Type | Surface Contact | Force as % of Flat-Plate Rating |
|---|---|---|
| Clean flat steel plate | Solid, full contact | 90 – 100% |
| Steel slab / billet (smooth top) | Good contact | 80 – 95% |
| Structural sections (H-beam, channel) | Irregular — air gaps | 50 – 70% |
| Light scrap (HMS No.2) | Loose, irregular | 40 – 60% |
| Heavy scrap (HMS No.1, shredded) | Dense, irregular | 35 – 55% |
| Steel pipe / tube | Curved — line contact | 45 – 65% |
Critical note for buyers: A magnet sized only to its flat-plate rated force will be severely underperforming on scrap or structural sections. For scrap handling applications, the magnet must be sized to achieve the required lifted weight at 40–55% of its flat-plate maximum. Always request a lifting force calculation based on your specific material — not a catalogue flat-plate rating.
Steel service centers receive large quantities of flat plate and structural sections, process to customer requirements, and dispatch to end users. Material moves through multiple stages — receiving, storage, feeding processing lines, finished goods handling, and loading outbound. Every stage involves repeated lifting, often of the same material multiple times.
A magnetic overhead crane with a rotating multi-magnet beam handles the complete flow. Incoming plate from a delivery truck is picked directly without slings — the magnet engages the full plate surface, the load is transferred to storage, and releases cleanly. Feeding a plasma cutting line requires precise placement onto a narrow cutting table; VFD-controlled slow hoisting speed provides the positioning precision needed. Loading outbound vehicles requires rapid, repeated cycling — the high duty cycle specification handles this without coil overheating.
Scrap yards are the highest-intensity magnetic crane environment. The crane operates near-continuously throughout every shift — picking from loose scrap piles, transporting to shredder feed conveyors, baling presses, or outbound trucks, and returning immediately for the next pick. Cycle times are short. The magnet is rarely fully de-energized.
The specification for this application is demanding:
A scrap yard magnet specified to standard plate-handling parameters will fail within the first operating year. The specification must be driven by the actual operating conditions — not by the easiest configuration to supply.
In steel mills, magnetic cranes handle billets, blooms, and slabs at various stages of production — continuous caster runout tables, cooling beds, rolling mill feed areas, and product storage. Some material is still hot when lifted.
Standard magnets are rated for material surface temperatures up to 100°C. Billet from a continuous caster or fresh from a rolling mill may be at 300–600°C. The specification for hot material requires:
Never assume a room-temperature lifting force rating applies to hot steel. Request the hot-material force calculation explicitly.
Shipyards and heavy fabrication workshops handle large steel plate panels and structural sections across wide bays — typically 20–35 metre spans. Electromagnetic cranes replace manual rigging teams that would otherwise be needed to sling each plate before every lift.
For large panel handling, a fixed or motorized multi-magnet beam prevents the plate from bending at the pickup point under a single central magnet. Anti-sway control on hoist and trolley drives is particularly important in shipyard environments — a large steel panel swinging freely in a busy fabrication bay creates serious risk and disrupts production.
The span and hook height specification must account for the full working area — from plate storage racks at one end of the bay to the assembly positions at the other, with sufficient hook height to clear the tallest workpiece in the travel path.
Steel rail is long, heavy, and difficult to rig conventionally. A standard rail section weighs 40–70 kg per metre. A 25-metre rail section weighs 1,000–1,750 kg and requires multiple sling attachment points, careful balancing, and a rigging crew to manage safely with a hook crane.
An electromagnetic crane with a multi-magnet beam — with magnet centres matched to the rail length — handles the full section in a single pick without any manual rigging. For facilities handling mixed rail profiles and lengths, an adjustable-centre beam allows the same crane to handle the full product range. The operational efficiency gain over sling-based rigging is significant in active track maintenance operations where rail volume is high.
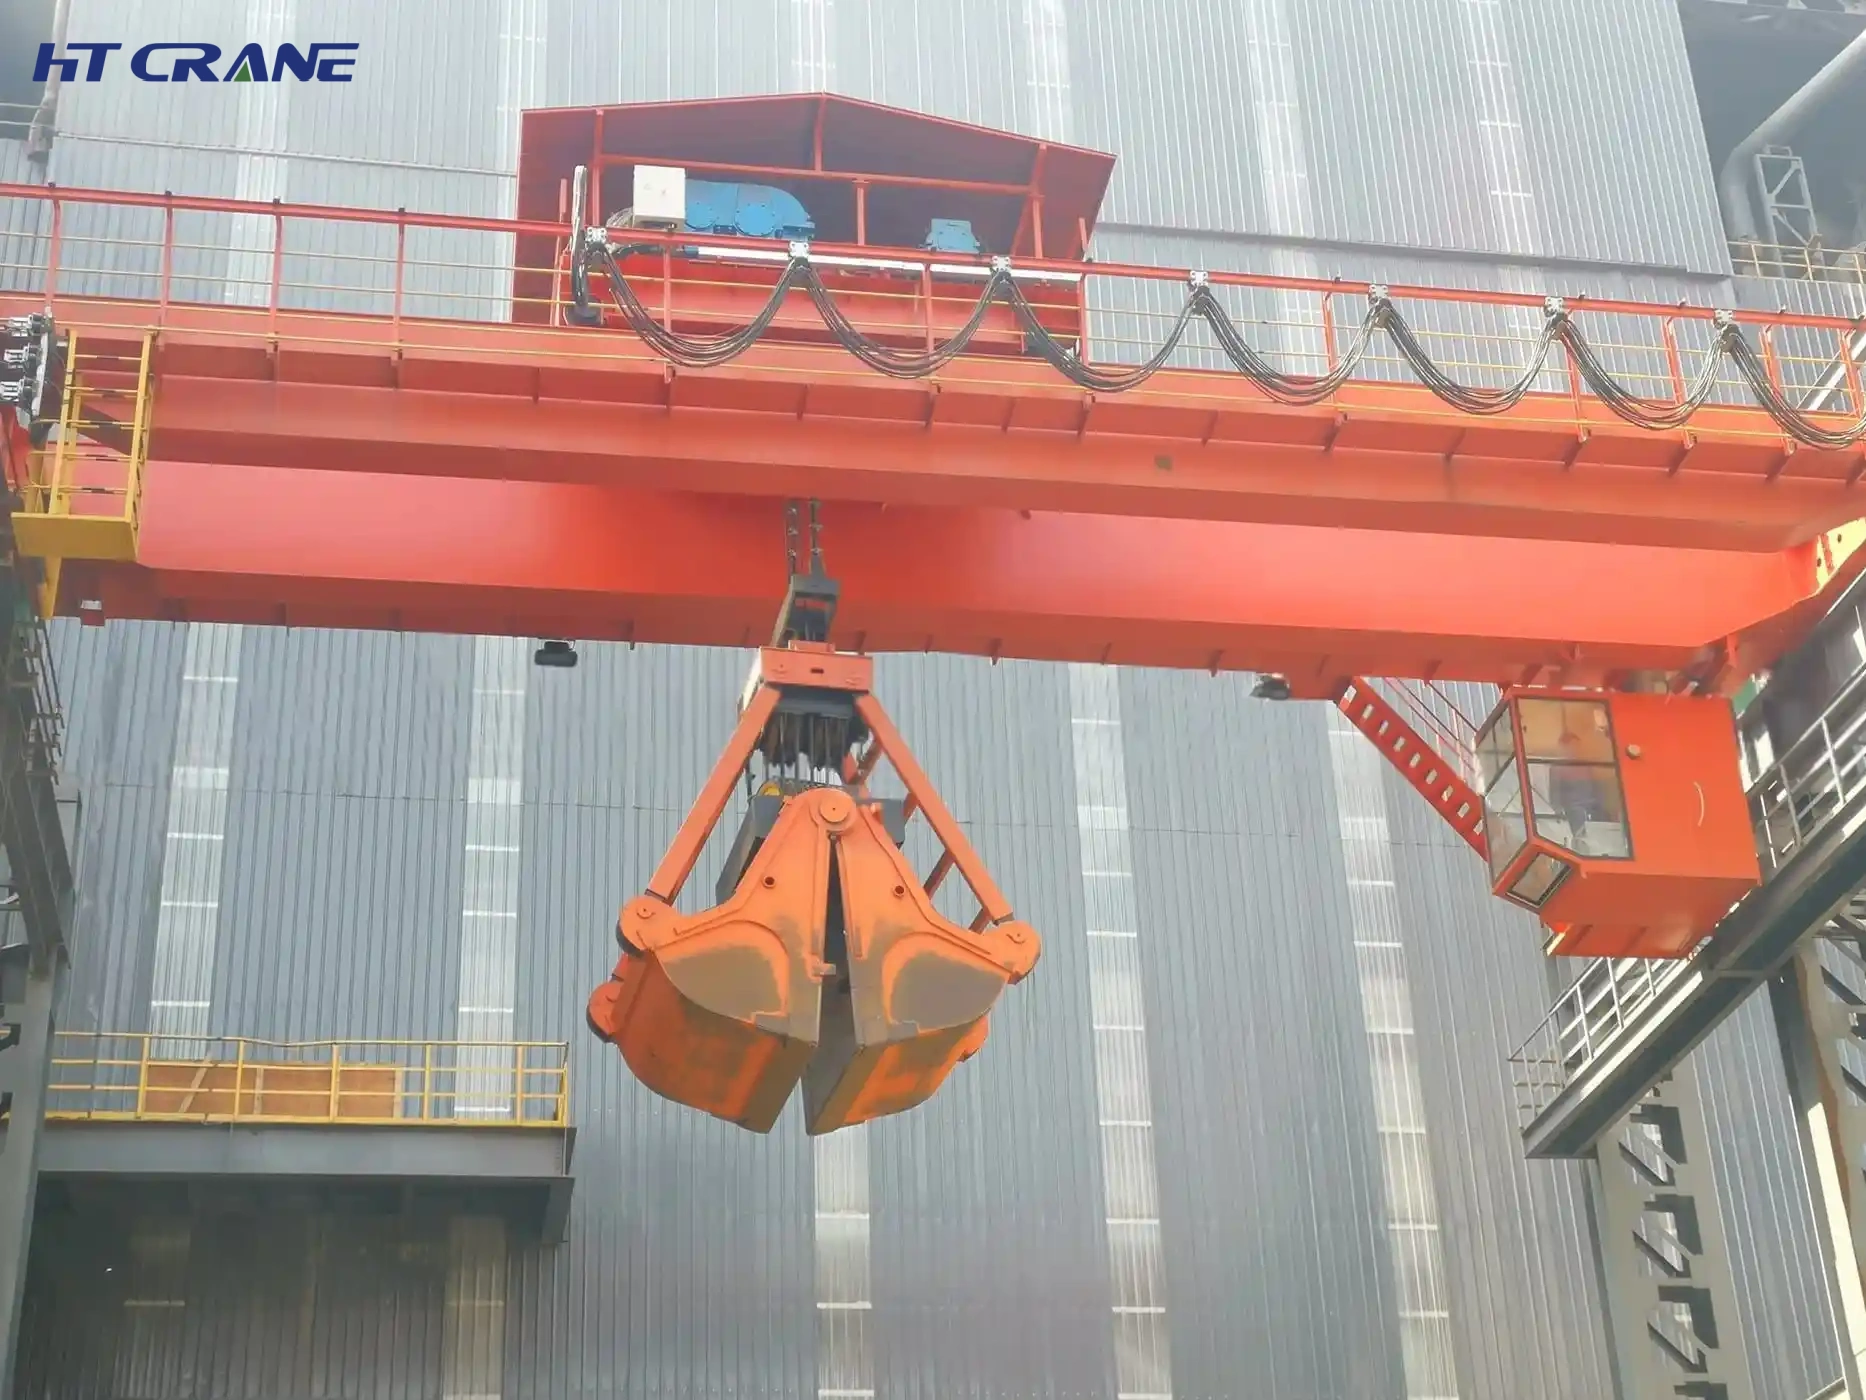
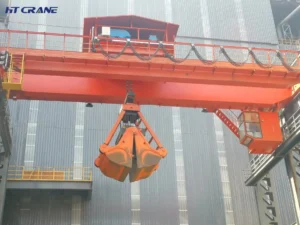
Manual rigging slows bulk material operations down and ties up labor that could be better used elsewhere. An overhead grab crane eliminates that problem entirely. The crane lifts, moves, and releases bulk material — coal, scrap metal, ore, sand, grain — without any manual load attachment. One operator handles the full cycle from the cabin. For facilities handling bulk materials repeatedly across a large floor area, an overhead grab crane is not just a convenience. It is the right tool for the job — designed from the structural level up for the high-cycle, high-wear demands of continuous bulk handling. A standard overhead crane running grab operations will reach the end of its structural fatigue life years ahead of schedule. A purpose-built grab crane is designed to last. This page gives you the full picture: what an overhead grab crane is, how the different grab types compare, what the key specifications mean, and what to verify before you commit to a purchase. What Is an Overhead Grab Crane? An overhead grab crane is a double girder overhead crane fitted with an…
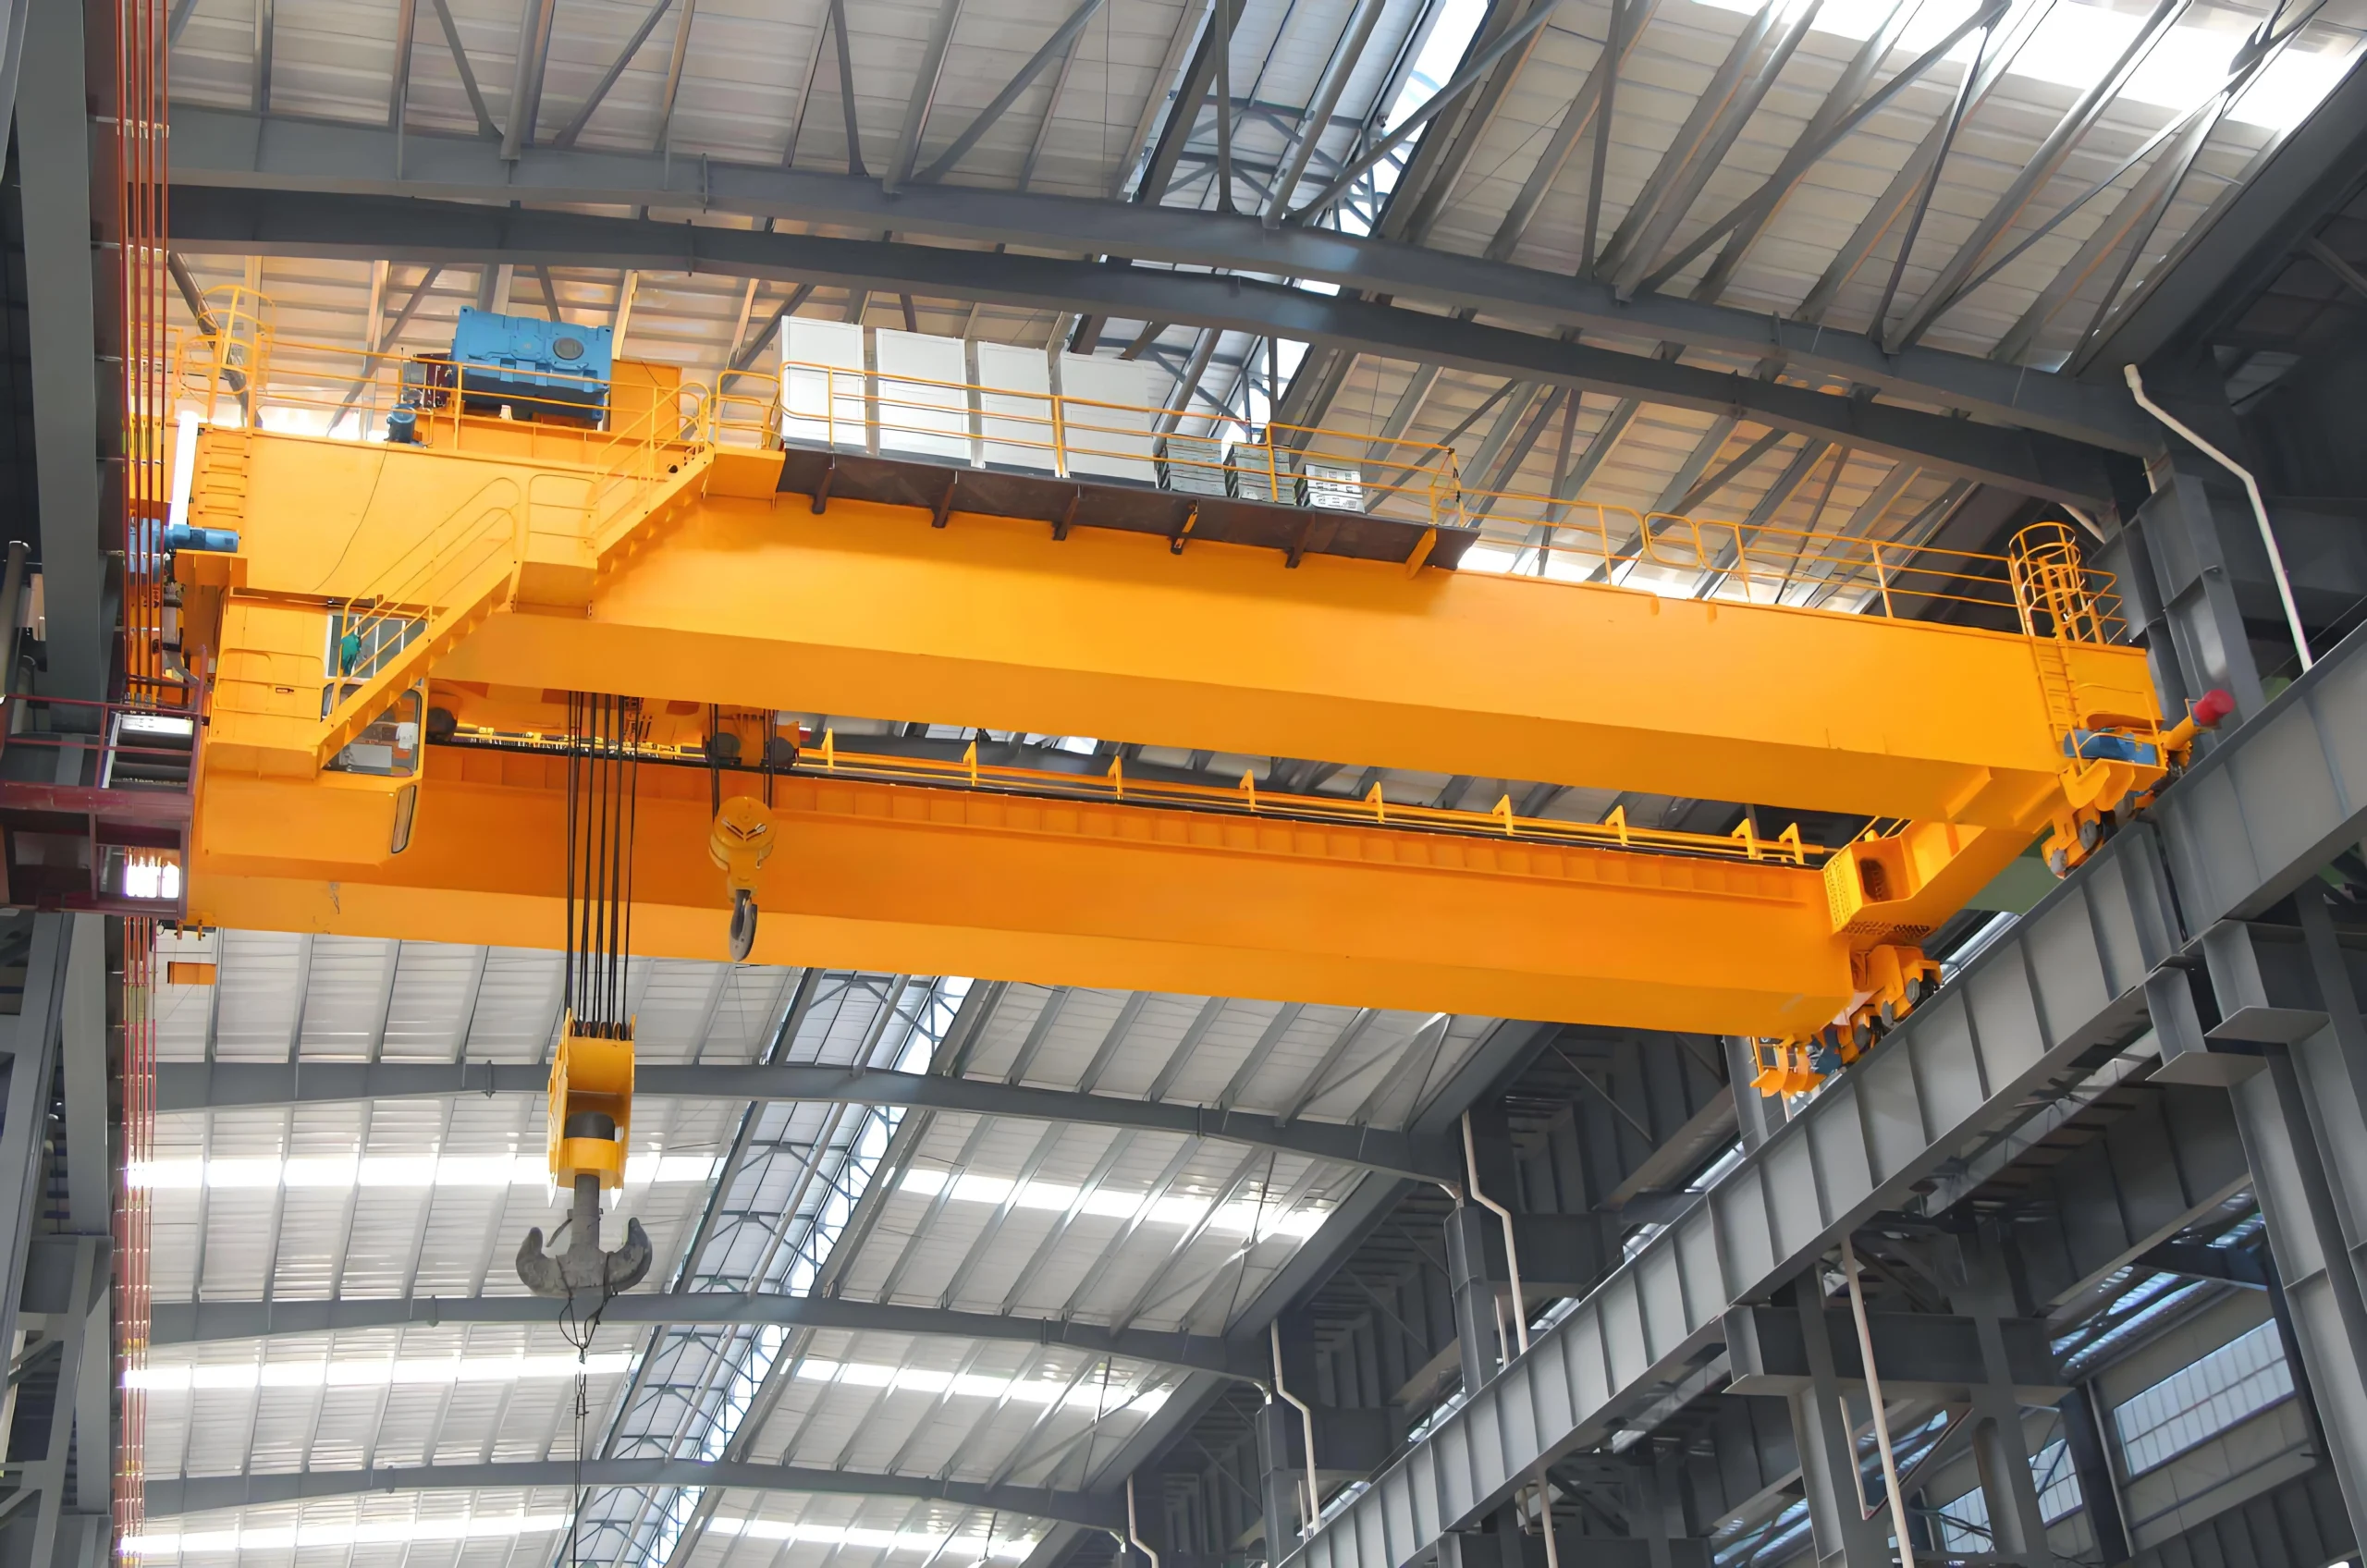
Because the load is too heavy, the span too wide, or the operating environment too demanding — a double girder overhead crane is the answer. Two main girders share the structural load, allow a top-running hoist trolley, and deliver the hook height, capacity, and duty cycle performance that heavy industrial operations require. The challenge for buyers is that “double girder overhead crane” covers multiple very different machine types. each is designed for a specific operating environment or load type. Specifying the wrong type creates safety risk, regulatory non-compliance, or a crane that fails prematurely because it was not built for the conditions it faces. This page covers six types in a single reference. By the end, you will know what distinguishes each model, where it belongs, and which one matches your operation — before you speak to any supplier. What Is a Double Girder Overhead Crane? The Structural Foundation A double girder overhead crane uses two parallel main girders spanning the building width. End trucks at each end run on elevated runway rails attached to the building structure. The hoist…